Industrial HDPE Pipes
Chemical-resistant PE100 HDPE pipes for industrial process lines, effluent systems, mining operations, and cable protection — where metal pipes fail.
63mm – 630mm
Diameter Range
PN 6 – PN 16
Pressure Classes
pH 1 – 14
Chemical Resistance
3–5× Steel
Abrasion Rating
PE100 Virgin Resin
Material Grade
IS 4984:2016 / ISO 4427
Standard

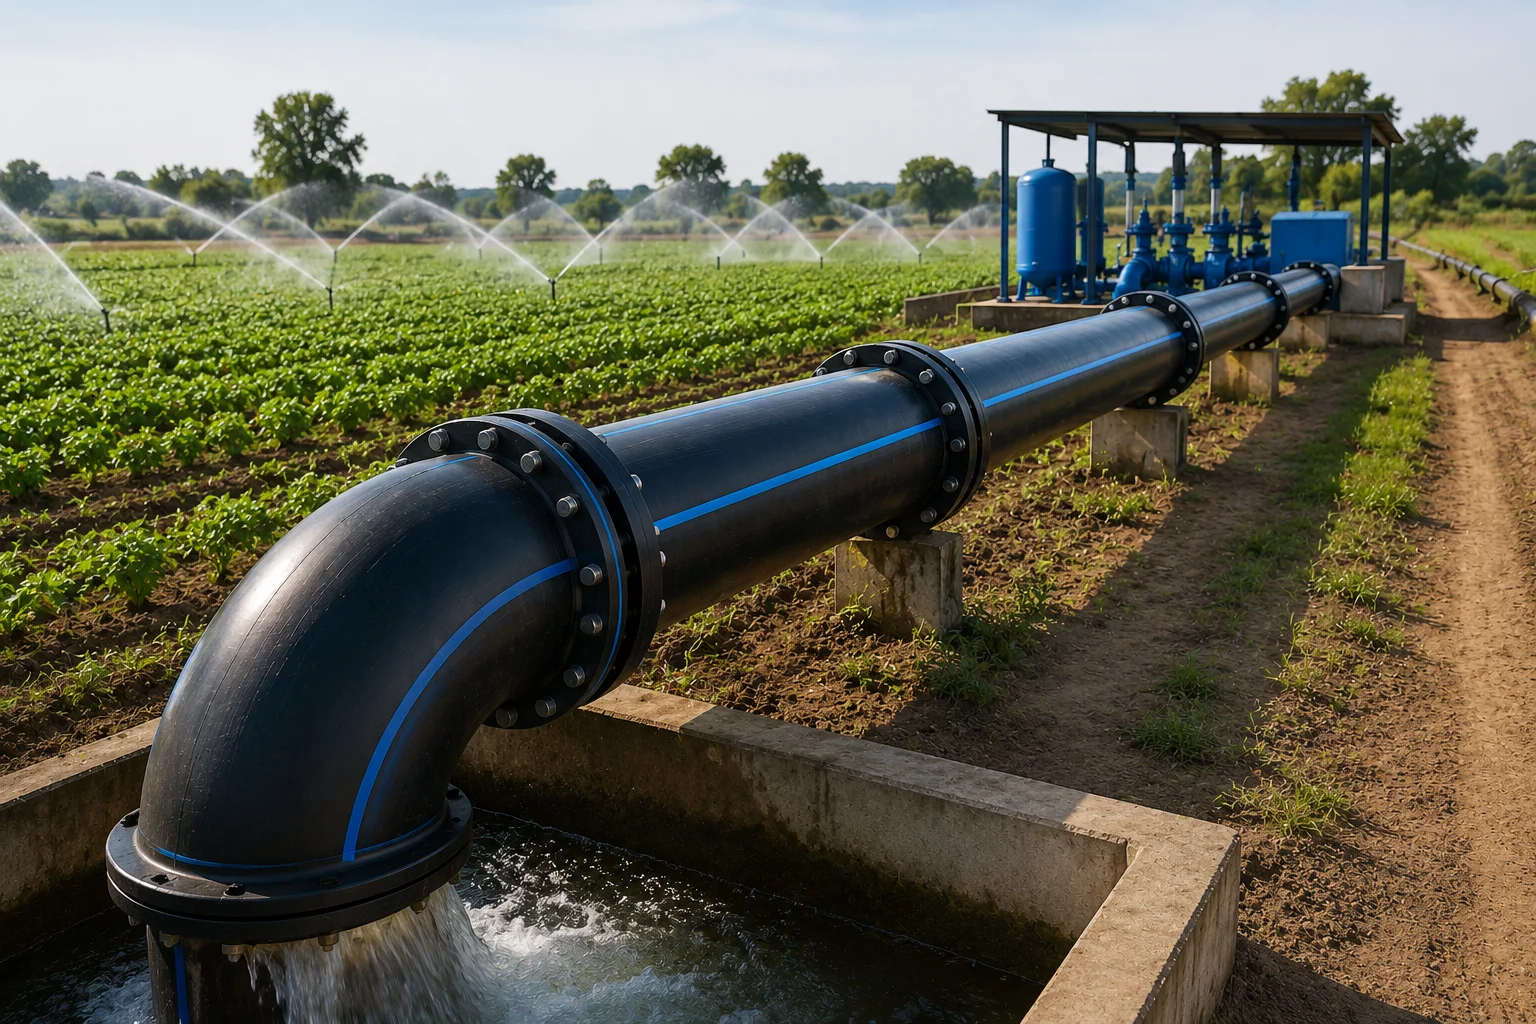
In industrial environments, pipes face challenges that destroy traditional materials: corrosive chemicals, abrasive slurries, extreme temperature cycles, and aggressive soil conditions. TARKO PE100 HDPE pipes thrive in these conditions — they resist a wide range of chemicals, handle abrasive flow without erosion, and operate maintenance-free for decades.
HDPE is inherently resistant to most acids, bases, and organic solvents encountered in industrial operations. Unlike metal pipes that corrode from inside and outside simultaneously, or concrete pipes that are attacked by acidic effluent, HDPE maintains its integrity across a pH range of 1–14. This makes it the material of choice for chemical process lines, acid drainage, industrial effluent, and leachate collection.
For mining and minerals processing, HDPE's abrasion resistance exceeds that of steel by 3–5×. Slurry pipelines carrying coal, fly ash, sand, and mineral tailings last significantly longer in HDPE than in MS or CI. The pipe's flexibility also allows it to accommodate ground settlement and vibration without joint failures.
TARKO supplies industrial HDPE pipes from 63mm to 630mm in PN 6 to PN 16, with larger diameters and higher pressures available on project-specific orders. We work directly with EPC contractors, MIDC estates, chemical plants, power utilities, and mining operations across India.
Why Choose TARKO Industrial HDPE Pipes?
Engineered for performance, certified for quality, priced for value.
Chemical Resistant
Resists acids, alkalis, and solvents across pH 1–14. Immune to electrochemical and galvanic corrosion that destroys metal pipes.
Abrasion Resistant
3–5× more abrasion-resistant than steel. Ideal for slurry, fly ash, and mineral transport where erosion destroys metal pipes.
Cable Ducting
Smooth bore, lightweight, and available in long coiled lengths — ideal for telecom, electrical, and fiber optic cable protection.
Industrial Grade Quality
PE100 virgin resin with full traceability. Every batch tested for MFR, density, and OIT. ISO 9001:2015 quality system.
Low Lifecycle Cost
50+ year life, zero maintenance, no cathodic protection needed. Total cost of ownership far lower than metal alternatives.
Effluent & Drainage
Leak-proof welded joints prevent environmental contamination. Meets requirements for effluent disposal and leachate management.
Applications
- Chemical process piping (acid, alkali, solvent)
- Industrial effluent disposal and ETP connections
- Mining — slurry, tailings, and dewatering
- Thermal power — fly ash disposal and cooling water
- Telecom and fiber optic cable ducting
- Electrical cable protection conduits
- MIDC/GIDC industrial estate water and drainage
Technical Specifications
| Diameter Range | 63mm – 630mm |
| Pressure Classes | PN 6 – PN 16 |
| Chemical Resistance | pH 1 – 14 |
| Abrasion Rating | 3–5× Steel |
| Material Grade | PE100 Virgin Resin |
| Standard | IS 4984:2016 / ISO 4427 |
Frequently Asked Questions
Common questions about Industrial HDPE Pipes
Related Products
Need Industrial HDPE Pipes? Get Factory-Direct Pricing
TARKO manufactures and supplies directly from our BIS-certified factory in Nagpur. No middlemen, no markups — just the best HDPE pipes at the best price.